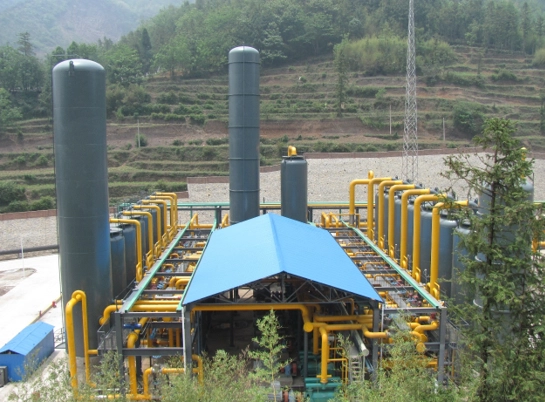
Methane concentration technology – gas
The company’s proprietary technology developed for low concentration gas, after fully analysing the nature of the raw gas, adopts variable pressure ad…
1. Product Overview
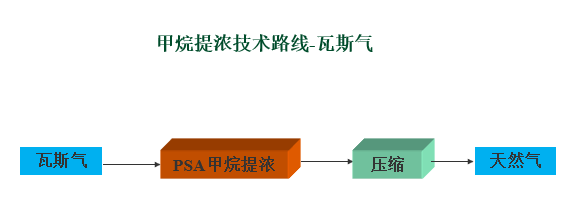
This system is designed for the treatment and concentration of oxygen-containing low-concentration coalbed methane. It adopts a micro-pressure Pressure Swing Adsorption (PSA) process to selectively separate methane (CH₄) from nitrogen (N₂) and oxygen (O₂).
Compared with conventional methods such as membrane separation, deoxygenation, and direct liquefaction, this system focuses on low-energy, low-pressure methane enrichment.
Developed by Chengdu Huaxi Chemical Technology Co., Ltd., the system is suitable for industrial-scale coalbed methane utilization and energy recovery.
2. Process Description
-
Feed gas: Oxygen-containing coalbed methane
-
Methane content range: 10–15% (typical), up to 30% applicable
-
Separation method: Micro-pressure PSA / Vacuum PSA optional
-
Output: Enriched methane gas for combustion or further upgrading
Process function:
-
One-stage concentration: ≥30% CH₄ for power generation fuel use
-
Two-stage concentration: Upgraded to natural gas quality
3. Equipment Capacity
-
Standard capacity range: 2,000 – 30,000 Nm³/h
-
Operating mode: Continuous or flexible load operation
4. Technical Features
4.1 Low Energy Consumption Operation
-
No high-pressure feed compression required
-
Low-pressure PSA operation reduces overall power consumption
-
Improved system safety due to reduced pressure risk
4.2 Adjustable Gas Purity Output
-
Methane concentration can be adjusted based on process requirements
-
Supports different end-use scenarios:
-
Boiler / combustion fuel gas
-
Power generation fuel
-
Pipeline-grade upgrading feed gas
4.3 Strong Feed Gas Adaptability
-
Applicable methane concentration range: 10% – 30% CH₄
-
Operating pressure: approximately 20 kPa (gauge pressure)
-
Supports vacuum PSA configuration for low-pressure gas sources
4.4 Wide Operating Range
-
Stable operation range: 30% – 110% load flexibility
-
Suitable for fluctuating coalbed methane production conditions
5. Application Scope
-
Oxygen-containing coalbed methane systems (CH₄ ≥ 10%)
-
Coal mine gas utilization projects
-
Low-concentration methane recovery and energy conversion systems
-
Industrial fuel gas upgrading systems
6. Output Gas Usage
-
Industrial boiler fuel
-
Gas turbine / power generation fuel
-
Further natural gas upgrading feedstock
-
Distributed energy systems
7. Manufacturer
Chengdu Huaxi Chemical Technology Co., Ltd.
Specialized in low-concentration methane separation, PSA gas purification systems, and coalbed methane utilization technologies.
Process Diagram
Typical Performance
|
No. |
User |
Raw Material |
Product |
Process Route |
|
1 |
Huainan Mining Group Xieyi Mine |
Coalbed Methane |
Methane > 95% |
Micro-pressure Vacuum Re-concentration Method |
|
2 |
Xinzhuangzi Mine |
Coalbed Methane |
Methane > 95% |
Micro-pressure Vacuum Re-concentration Method |
|
3 |
Panjiang Coal and Electricity Group Jinjia Mine |
Coalbed Methane |
Methane > 95% |
Micro-pressure Vacuum Re-concentration Method |
Related products
-
High-Vacuum Fume Extraction
Contact UsHigh-Vacuum Fume Extraction Solutions for Precision Industrial Applications
-
Hazardous Waste Incineration Device for Hubei Shengling
Contact UsThis project intends to build a hazardous waste incineration device of 80t/d wastewater, 6.0t/d waste liquid, 11000Nm3/h waste gas and 500kg/d solid waste of Hubei Shengling Technology Co., Ltd., which is used to incinerate and treat hazardous waste generated by the plant.
-
High Voltage Energy Storage Cabinet 512V Series Industrial Grade Battery System
Contact UsThe 512V high-voltage energy storage cabinet is an industrial-grade battery system designed for stable backup and hybrid solar energy storage. It supports high-power discharge, modular expansion, wide
-
DF-03 HT Modified Starch
Contact UsDF-03 is modified starch by inserting hydration groups and high temperature stabilizer to improve the water solubility and temperature resistance (up to 135 ℃). And ensure its good fluid loss performance under both low and high temperature. DF-03 is an environmental friendly, low viscosity, salt resistance (up to saturation) filtration reducer. Its recommend dosage is 1.0%-2.0%.
Reviews
There are no reviews yet.